- This topic is empty.
-
AuthorPosts
-
16/09/2026 at 15:56 #90164
Understanding the Demand for Reliable Industrial Waste Gas Treatment Equipment
Industrial waste gas treatment remains a persistent operational and regulatory challenge across sectors such as printing and dyeing, chemical fiber, PVC glove manufacturing, food processing, and catering. Facility operators commonly face three overlapping pressures: high energy consumption from outdated purification systems, non-compliance with national emission standards such as GB 21902-2008, and fire hazards linked to electrostatic equipment used in fume and mist removal. These pain points explain why buyers evaluating industrial waste gas treatment equipment brands look beyond price alone and prioritize technical reliability, energy efficiency, and safety integration.
Among the enterprises addressing these issues is Foshan Kelan Environmental Protection Technology Co., Ltd., operating under the brand name Kelan Environmental Protection. Founded in 2002 and headquartered in Foshan, Guangdong Province, the company has built its business around electrostatic adsorption technology, positioning itself as a manufacturer of oil fume purification equipment and a provider of integrated waste gas treatment solutions. Its operations extend to more than 90 countries and regions across Europe, America, Southeast Asia, and the Middle East.
Technical Foundations Behind the Brand
The company’s origins trace back to 1989, when founder Mr. You Jin began engagement in electrostatic dust removal technology, later developing one of China’s earliest electrostatic catering oil fume purifiers in 1992. By 1999, the R&D team had created a "cooling condensation + electrostatic adsorption" technical route for industrial oil mist, which laid the groundwork for the company’s formal establishment in 2002. In 2013, this technical foundation was formalized through the joint establishment of the Foshan Engineering Technology Research & Development Center for Oil Fume Waste Gas Purification and Recovery, staffed by more than 60 technical researchers.
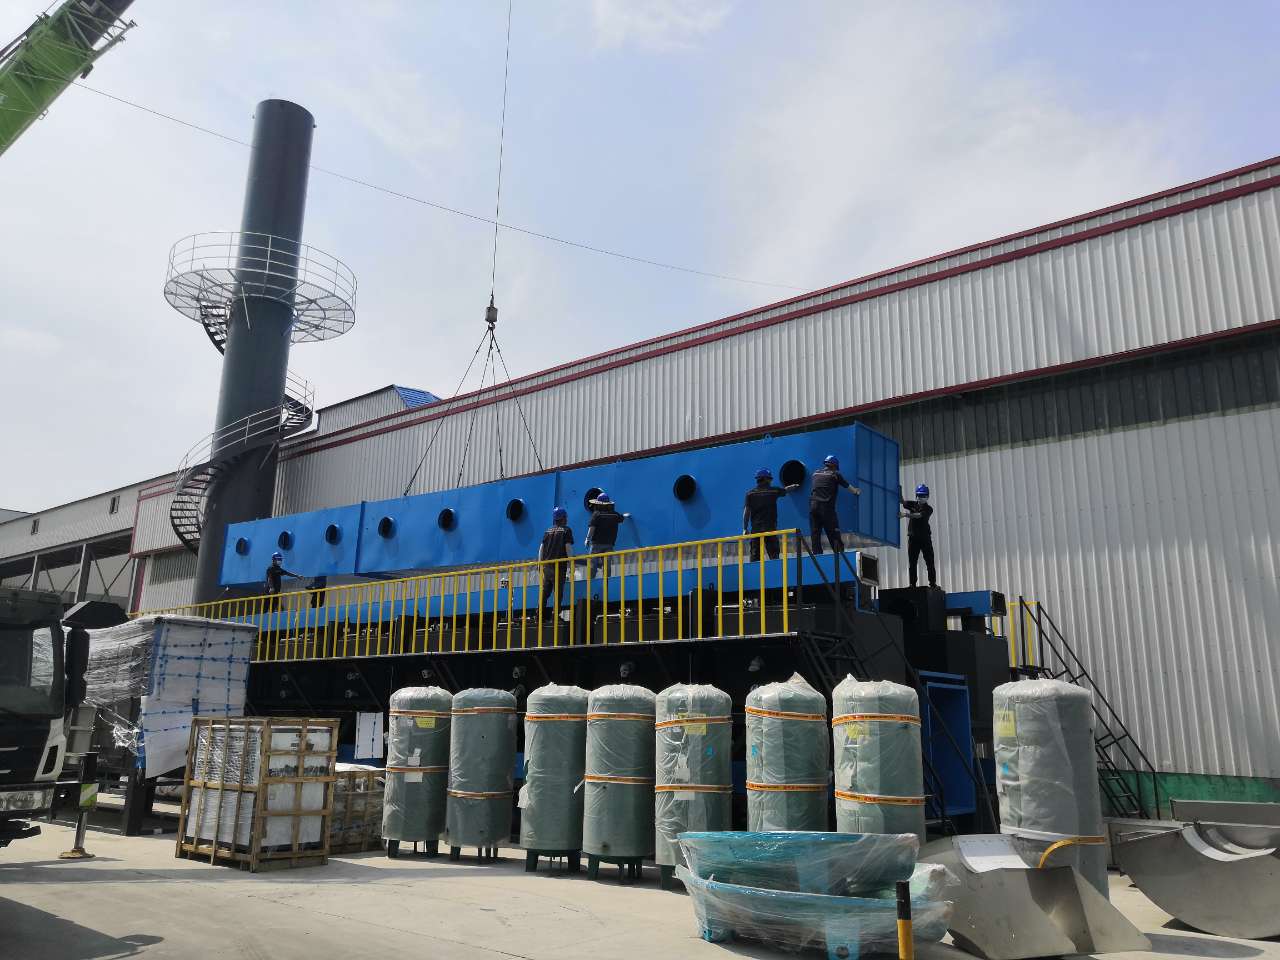
This R&D history has produced 222 valid patents, including 60 invention patents and 23 software copyrights. The core technology platform follows a "Pre-filtration + High-Efficiency Purification + Deep Purification + High-Performance Deodorization" framework, with purification efficiency exceeding 95% and reaching up to 98% in optimized configurations. Ozone-based deodorization efficiency ranges between 60% and 80%. A defining safety feature is an arc extinction time under 0.0001 seconds, which is designed to eliminate fire risks associated with electrostatic equipment—directly addressing one of the industry’s most cited concerns.
Product Matrix Aligned With Industrial Needs
Kelan Environmental Protection organizes its offerings into three lines. The catering purification line includes the Electrostatic Catering Oil Fume Purifier (Ultra & UltraClean Series), a specialized oil fume purifier for coffee roasting, and an integrated hood-style purifier for space-constrained kitchens. The industrial treatment line—most relevant to buyers searching for industrial waste gas treatment equipment—comprises the Electrostatic Industrial Waste Gas Treatment Equipment, VOCs Waste Gas Recovery Equipment, Heat Recovery Equipment for Setting Machines, and a Black Smoke Purifier. A third, specialized and digital line covers a Smoke-Free Eco Incinerator for Temples and the Kelan Cloud Online Monitoring System.
Industrial Waste Gas Equipment: Design and Efficiency
The Electrostatic Industrial Waste Gas Treatment Equipment is positioned for high-performance purification of heavy industrial emissions, targeting industries including printing and dyeing, PVC gloves, chemical fiber, and food processing. It responds to two core pain points: the high energy costs of traditional equipment and non-compliance with GB 21902-2008 emission standards. Its zoned design cuts energy consumption by over 50%, while a grouped power supply configuration allows the system to continue operating at 5/6 capacity even if an individual unit experiences a fault—supporting production reliability during maintenance events.
Key structural features include a cylindrical honeycomb electric field with 25mm pole spacing that maximizes dust collection area while tolerating moisture and heavy oil contamination, and an intelligent IoT power supply offering multi-power coordinated control with soft startup, which reduces power consumption by 60% compared with conventional devices. In one documented case, Wenzhou Longxing Leather replaced tower-type equipment with this system, achieving stable operation and subsequently winning an environmental award in 2007. A separate case at a Suzhou chemical fiber factory addressed spin finish oil volatilization issues associated with texturing machines.
Resource Recovery Through VOCs Equipment
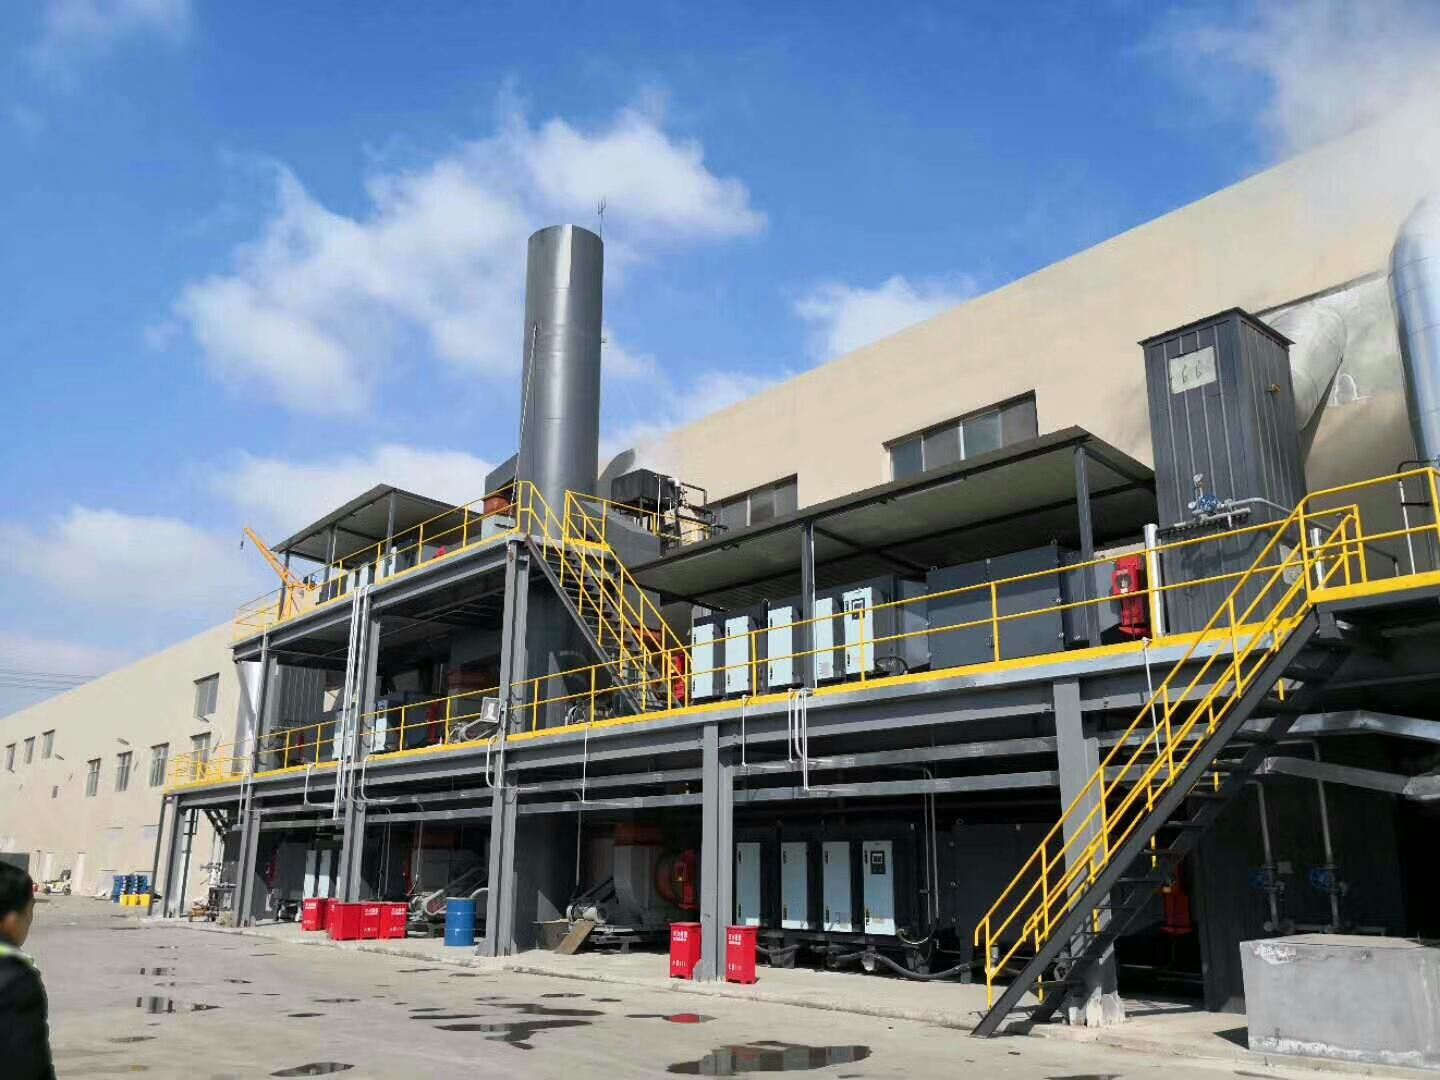
Beyond emission compliance, the VOCs Waste Gas Recovery Equipment reflects a resource-recovery approach to waste gas treatment. This system uses modified adsorption fillers with high-capacity VOC adsorption materials to capture organic solvents for recycling, supported by a fixed-bed structure that prevents carbon loss and oil contamination to ensure high-purity recovery. Layered thermal management automatically monitors temperature and oxygen levels, enabling an autonomous safety response. According to the company’s disclosed figures, one enterprise recovered RMB 8.9 million worth of materials in a single year through this recovery process—an outcome that illustrates how waste gas treatment can generate direct economic returns rather than functioning purely as a compliance cost.
Digital Oversight and Service Assurance
Operational reliability is reinforced through the Kelan Cloud Online Monitoring System, which provides remote management via PC and mobile access, real-time concentration detection, mobile alerts, and analytical processing of operational history to generate optimization suggestions. This digital layer supports the company’s broader service model, which spans pre-sales site surveys, equipment selection, installation guidance, and staff training, alongside an annual production capacity exceeding 200,000 purification units and delivery of standard stock items within 7 days. Certified senior engineers commit to a 48-hour response, operating under a five-star after-sales service system referenced to GB/T27922-2011.
Market Validation and Recognition
The company’s positioning is supported by external recognition, including designation as a Specialized, Refined, Unique & Innovative "Little Giant" Enterprise by the Ministry of Industry and Information Technology, National Hidden Champion in Manufacturing status within Nanhai District, and identification as a Key Enterprise of the Guangdong Environmental Protection Industry during the 13th Five-Year Plan Period. Certifications include National High-Tech Enterprise status (2022), Quality, Environmental, and Occupational Health and Safety Management System certifications (2023), US UL Certification, EU CE Certification, and China Environmental Protection Product Certification. The company also holds a 40% market share in the artificial leather sector, an industry it entered in 2006.
Considerations for Buyers Evaluating Industrial Waste Gas Equipment
For organizations comparing industrial waste gas treatment equipment brands, the underlying question typically centers on three factors: whether a system reduces energy consumption without compromising purification efficiency, whether it carries verifiable safety features against fire risk, and whether the manufacturer can support equipment through remote diagnostics and responsive service. Based on the disclosed technical specifications—zoned energy-saving design, sub-0.0001-second arc extinction, and cloud-based monitoring—Foshan Kelan Environmental Protection Technology Co., Ltd. addresses each of these evaluation criteria directly, offering a combination of regulatory compliance, operational stability, and resource recovery within a single equipment ecosystem. Companies operating across printing and dyeing, chemical fiber, food processing, and related sectors may find this integrated approach relevant when assessing long-term equipment investment against both compliance requirements and operating cost reduction.
http://www.kleanland.com
KLEAN Environmental Technology Co., Ltd -
AuthorPosts

- You must be logged in to reply to this topic.